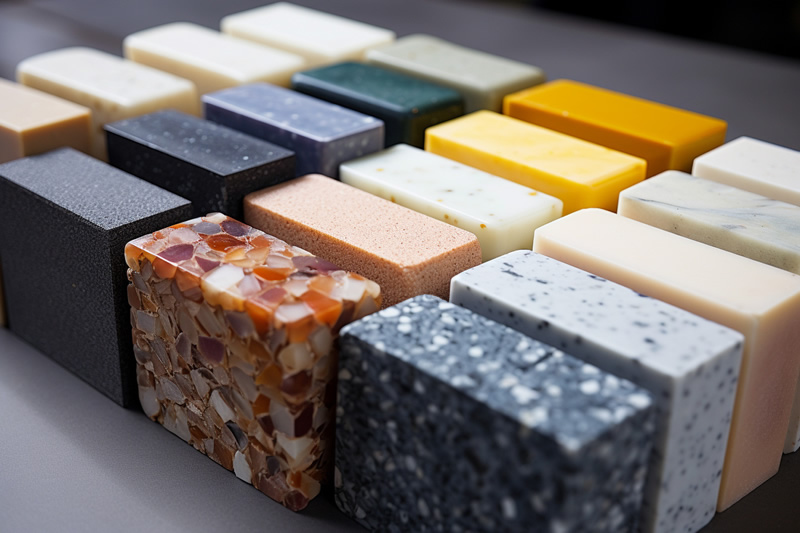
High-quality natural building materials are more popular than ever before. The floors of prestigious administrative buildings, airports, banks, and insurance companies all use marble or granite products with an elegant appearance.
The walls, ceilings, and facades of buildings are covered with expensive stone panels.
When processing stone, from the cutting stage to the final polishing stage, modern high-performance machines are used. Most machines rely on conveyor and processing belts, mainly due to their robustness and precision.
Monty belts dedicated to stone can meet these requirements.
Monty stone conveyor belts have low elongation, mainly attributable to the SD value of 60 N/mm belt width, measured at an installation elongation of 1%: robust and durable, their fabric structure ensuring smooth and continuous processing operations; dimensionally stable, even when humidity and temperature fluctuate; laterally rigid, so even wide belts stay flat; antistatic, avoiding static buildup.
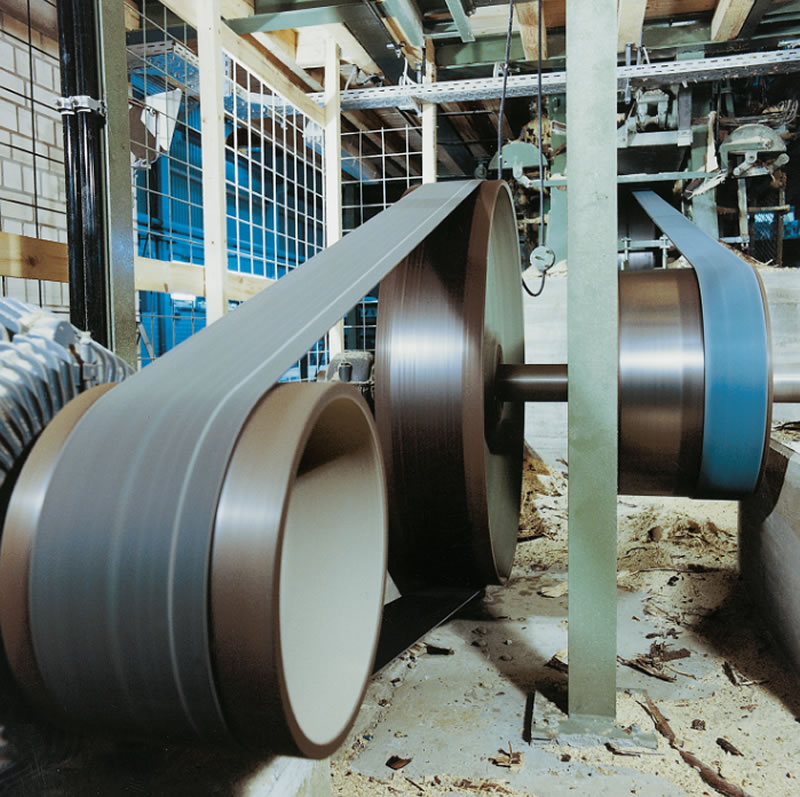
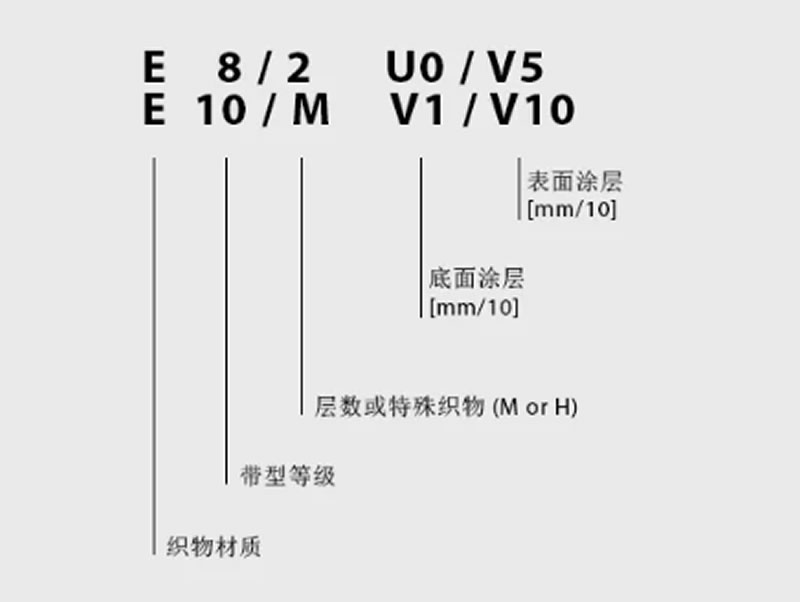
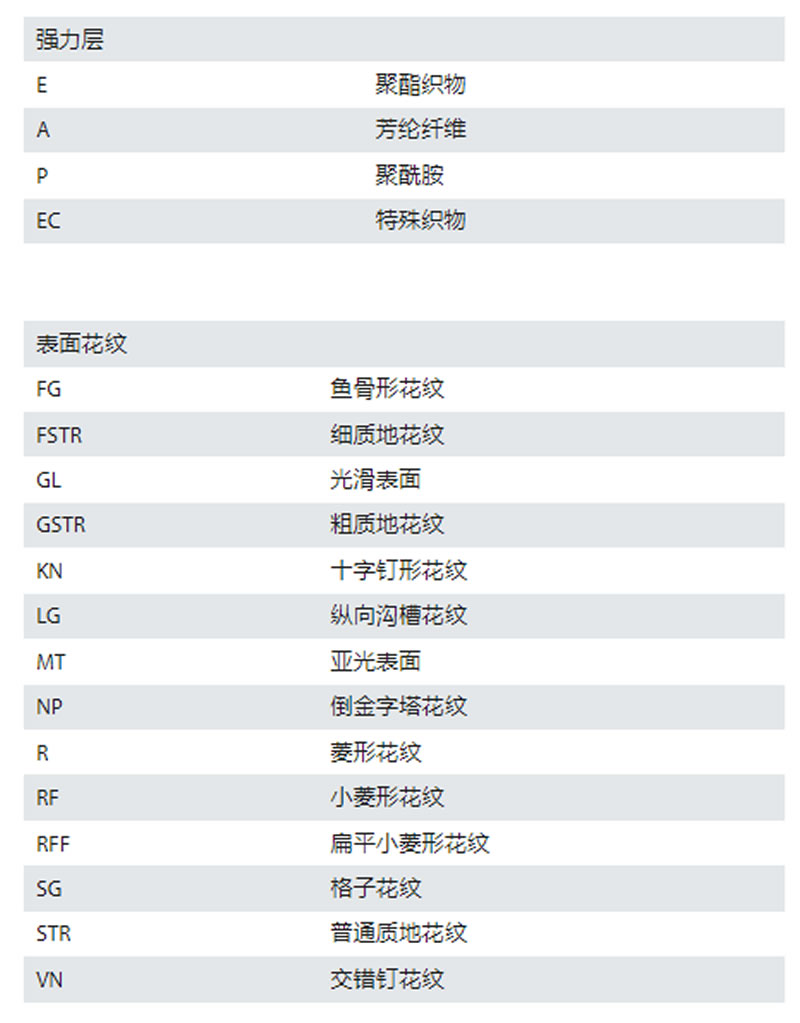
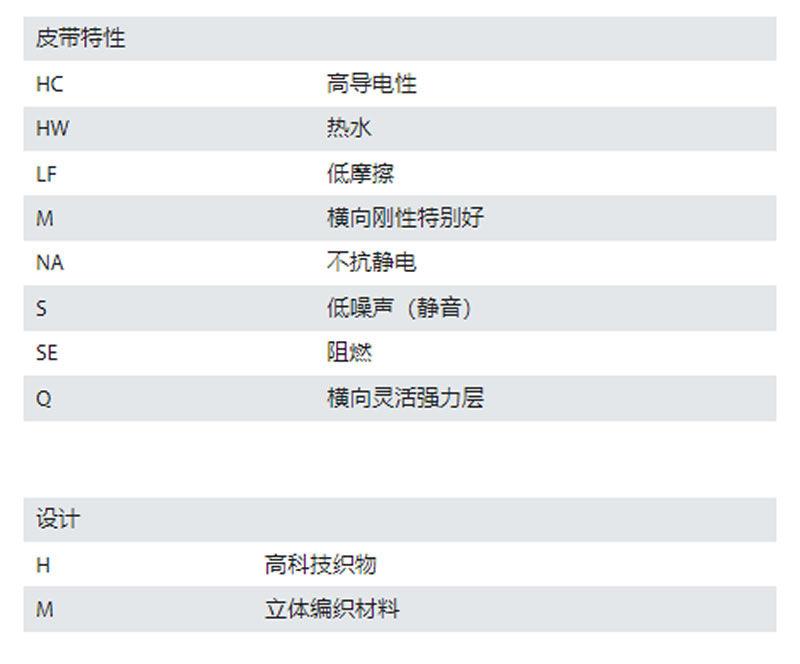
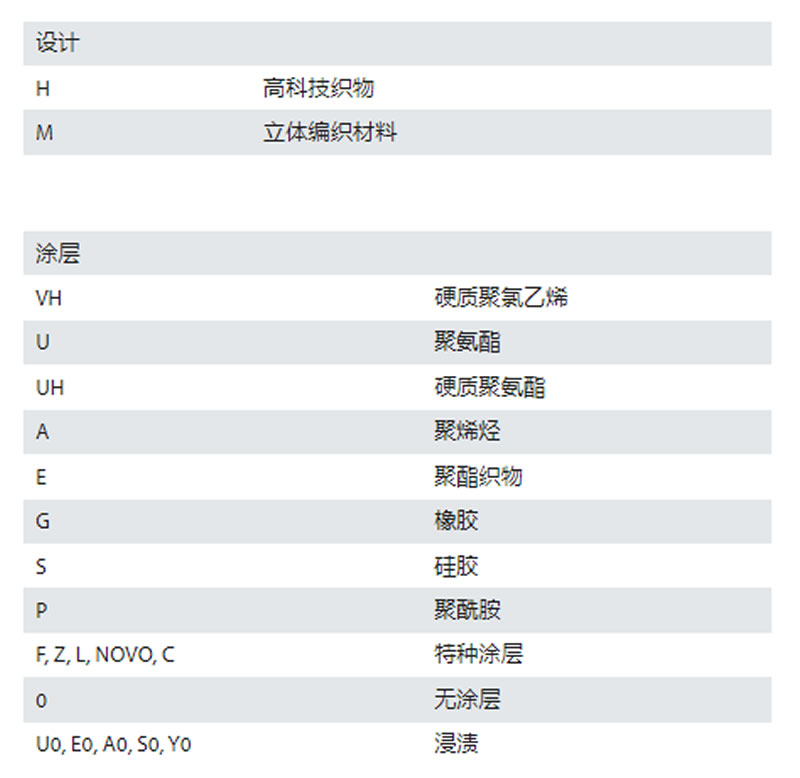
Monty stone conveyor belts with a rubber coating (model E9861) have the following features: particularly wear-resistant and durable, with a long service life and extremely high operating reliability; because of the high friction, they are particularly precise, and stone slabs will not slip even in an environment with water; G-coated belts are available in widths up to 2,200 mm without longitudinal splicing. Monty — Model Description
 Technical Consultation
 Sales Consultation