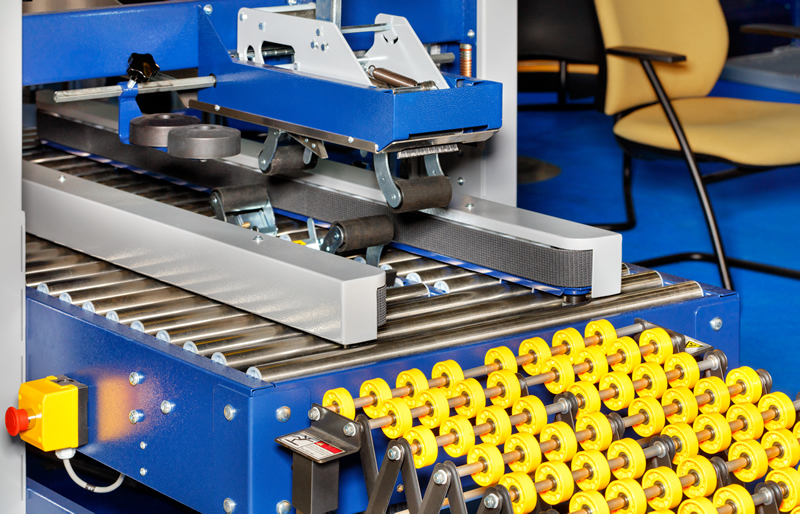
In this section, in addition to traditional food packaging machinery, other systems such as buffer systems, weighing, robots (vision sorting systems), or case conveying systems are also part of the packaging area. Monty belt solutions are highly innovative to match different applications and belt requirements.These inc...
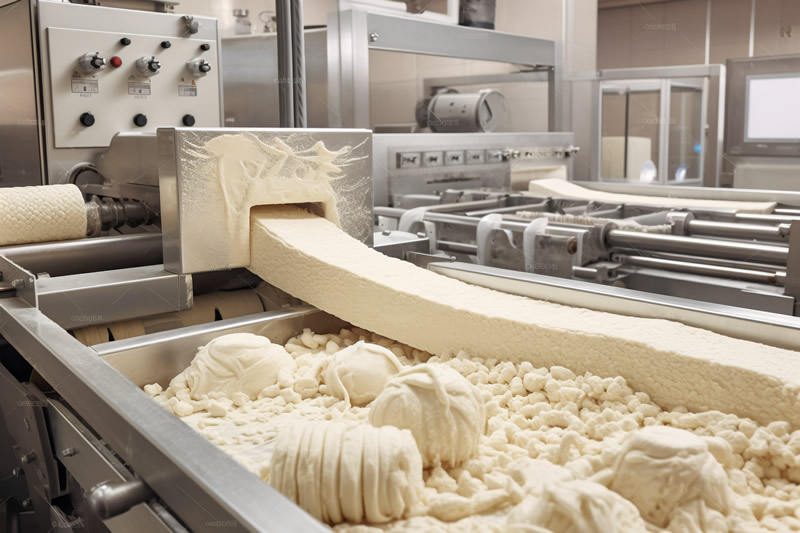
Food conveyor belts are widely used in the food industry. Their main function is to transport and convey food, ensuring the smooth processing and transportation of food.They are an efficient, continuous conveying tool, particularly suitable for material transport in food processing enterprises. Based on close partnersh...
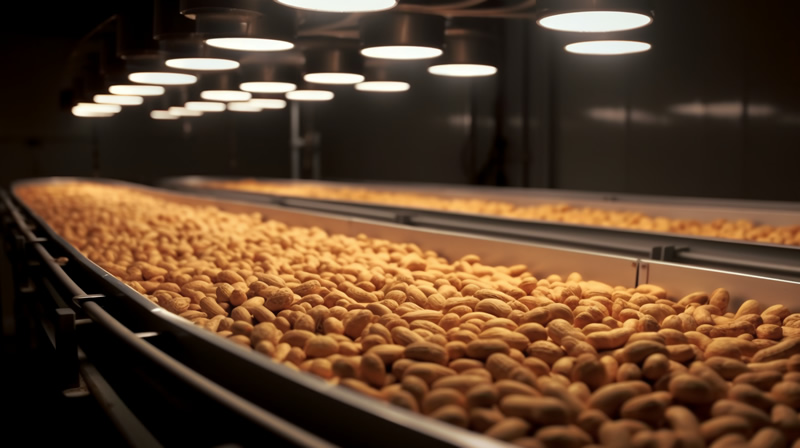
After harvesting, agricultural products such as fruit and vegetables need to be conveyed, washed, processed, and packaged on belts.The Monty range of conveyor belts and modular belts consists of powerful conveyor belts and is an excellent choice for these industrial processing operations. Steps such as washing, juice e...
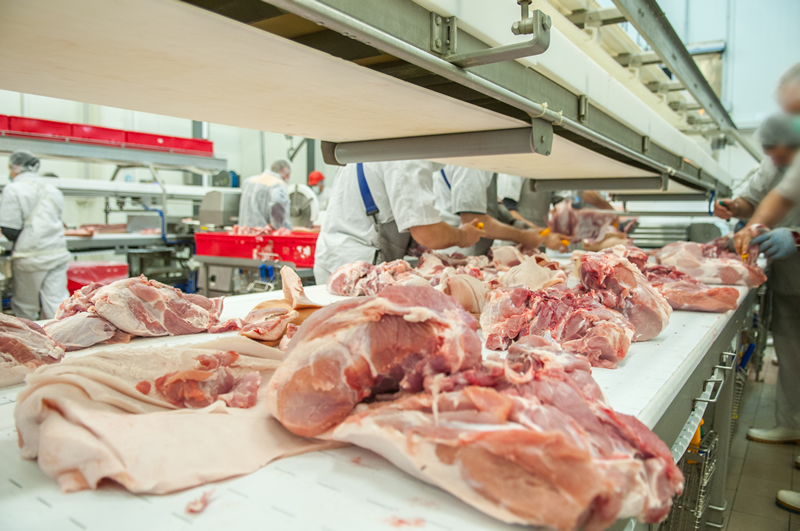
When handling meat, poultry, and seafood, hygiene requirements have the highest priority. Therefore, conveyor and processing belts must meet the requirements. Monty belts are the ideal choice for this industry, whether the belts have a fabric layer or not, or are plastic modular belts, or belong to the homogeneous belt...
The production and processing of milk and dairy products (such as cheese or butter) take place under very complex production conditions.Products with high water content, or products in which bacterial or mold cultures are commonly present, determine the special requirements for the belt. In addition to fabric conveyor ...
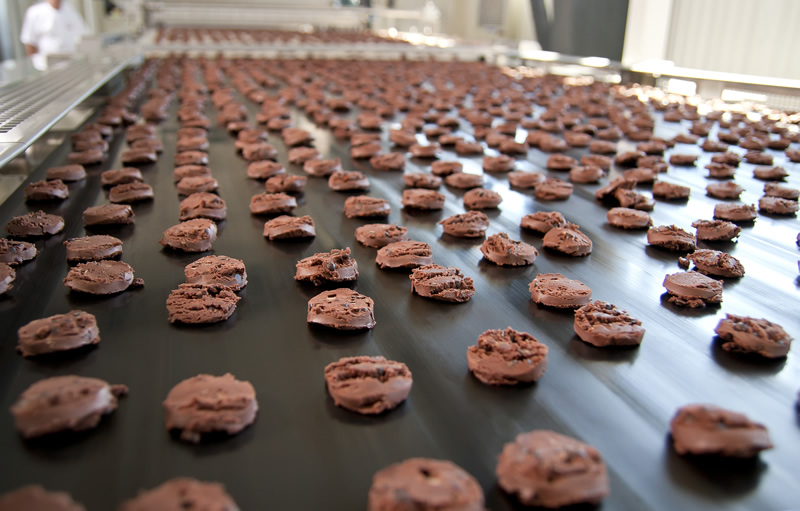
For sticky, greasy products such as all kinds of chocolate or gummy candy, special surface coatings or surface patterns are required during their production process.Monty conveyor and processing belts are suitable for multiple applications in the confectionery industry, ensuring reliable product conveying.
 Technical Consultation
 Sales Consultation