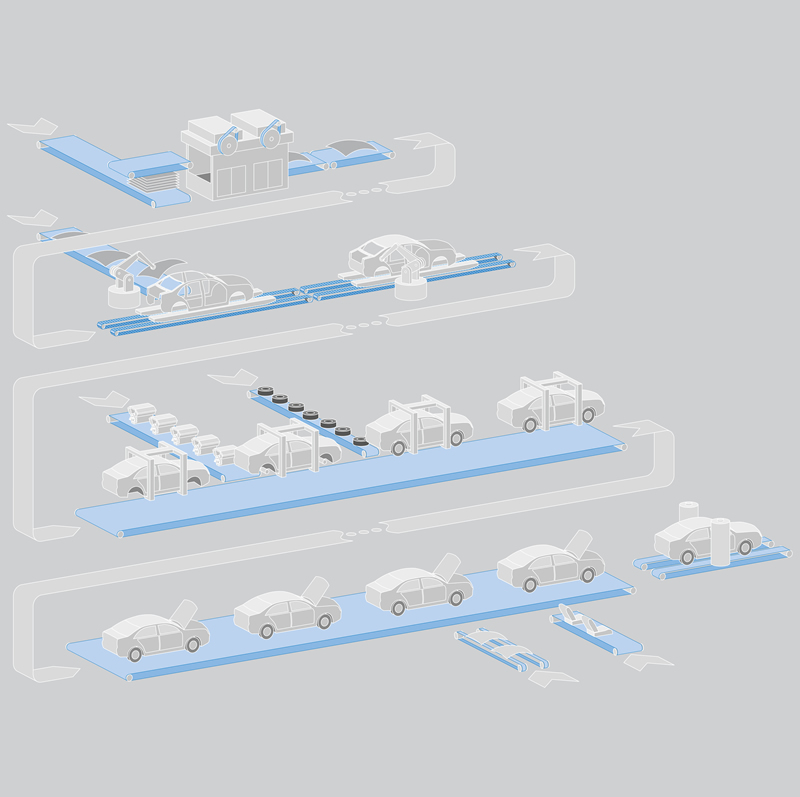
Automotive manufacturers and component suppliers (excluding tires).
Today, Monty conveyor belts and modular belts have replaced the thick rubber belts formerly used as personnel conveyor belts.
The combined advantages of these two product lines mean that conveyors are more compact and more cost-effective to operate. With the continuous development of the automotive industry and the sustained increase in demand, the requirements for production processes have also risen sharply. To respond to this trend, production machinery needs to operate very effectively and perfectly. The correct choice of conveyor belt plays a decisive role. If chosen correctly, machinery can run at full load. As a conveyor belt supplier, we can use our industry expertise to advise you on your conveyor belt selection.
For example, our Monty modular belt Series 7 and 8 offer the following decisive features: extremely high strength; robust, wear-resistant, and resistant to deformation; flame-retardant products are available as required — these products are certified through "flame-retardant flooring systems" (formerly B1), in compliance with Part 1 of the DIN EN 13501 standard, and/or conductive (resistance < 10⁶ Ω); special designs are available for users to choose from, such as anti-slip surfaces and wheel stops, with an open area of up to 25%.
 Technical Consultation
 Sales Consultation